About Sorbitol 70%
Sorbitol 70%
Sorbitol, a polyol (sugar alcohol), is a bulk sweetener found in numerous food products. In addition to providing sweetness, it is an excellent humectant and texturizing agent. Sorbitol is about 60 percent as sweet as sucrose with one-third fewer calories.
Versatile Industrial ApplicationsSorbitol 70% is a multi-functional ingredient ideal for industries requiring a humectant, sweetener, or thickener. Its compatibility with various manufacturing processes makes it a preferred choice for food processing, pharmaceuticals, cosmetics, and other industrial uses where moisture retention and a sweet profile are essential.
Strict Quality and Safety StandardsProduced and supplied under stringent BP/USP/EP/FCC standards, Sorbitol 70% is allergen-free, non-GMO, and low in heavy metals. Its microbial status adheres to the most demanding food and pharma requirements, ensuring it is safe for diverse end-uses. The product is non-toxic, odorless, and boasts a long shelf life.
Optimal Storage and Packaging SolutionsFor convenience and product integrity, Sorbitol 70% comes packaged in HDPE drums, IBC tanks, and bulk containers. Storing the syrup in a cool, dry place and tightly closed containers preserves its quality for up to 24 months from the manufacturing date, minimizing the risk of contamination or degradation.
FAQ's of Sorbitol 70%:
Q: How should Sorbitol 70% be stored to ensure maximum shelf life?
A: Sorbitol 70% should be stored in a cool, dry place in tightly closed containers. This helps maintain its quality and stability, allowing for a shelf life of 24 months from the manufacturing date.
Q: What are the primary industrial uses of Sorbitol 70%?
A: Sorbitol 70% is primarily used as a humectant, sweetener, and thickener in various industries, including food processing, pharmaceuticals, and cosmetics. It is valued for its moisture-retaining properties and sweet taste.
Q: Is Sorbitol 70% compliant with food and pharmaceutical safety standards?
A: Yes, Sorbitol 70% meets strict food and pharma microbiological specifications and is produced according to BP/USP/EP/FCC standards. It is also allergen-free, non-GMO, and contains low levels of heavy metals.
Q: What forms and packaging options are available for Sorbitol 70%?
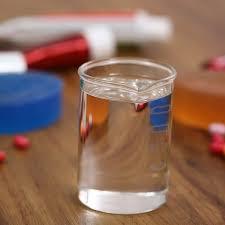
A: The product is supplied as a clear, syrupy liquid and is available in HDPE drums, IBC tanks, and bulk containers. This ensures flexibility and convenience for industrial-scale applications.
Q: Can Sorbitol 70% be used in formulations that require allergen-free and non-GMO ingredients?
A: Absolutely, Sorbitol 70% is both allergen-free and produced from non-GMO sources, making it suitable for sensitive formulations and strict labeling requirements.
Q: What benefits does Sorbitol 70% offer in industrial processes?
A: Sorbitol 70% enhances products by providing sweetness, moisture retention, and viscosity control. Its solubility in water, stable pH, and non-toxic nature support broad industrial usage.
 Send Inquiry






 Send Inquiry


 Send Inquiry
 English
 Spanish
 French
 German
 Italian
 Chinese (Simplified)
 Japanese
 Korean
 Arabic
 Portuguese
